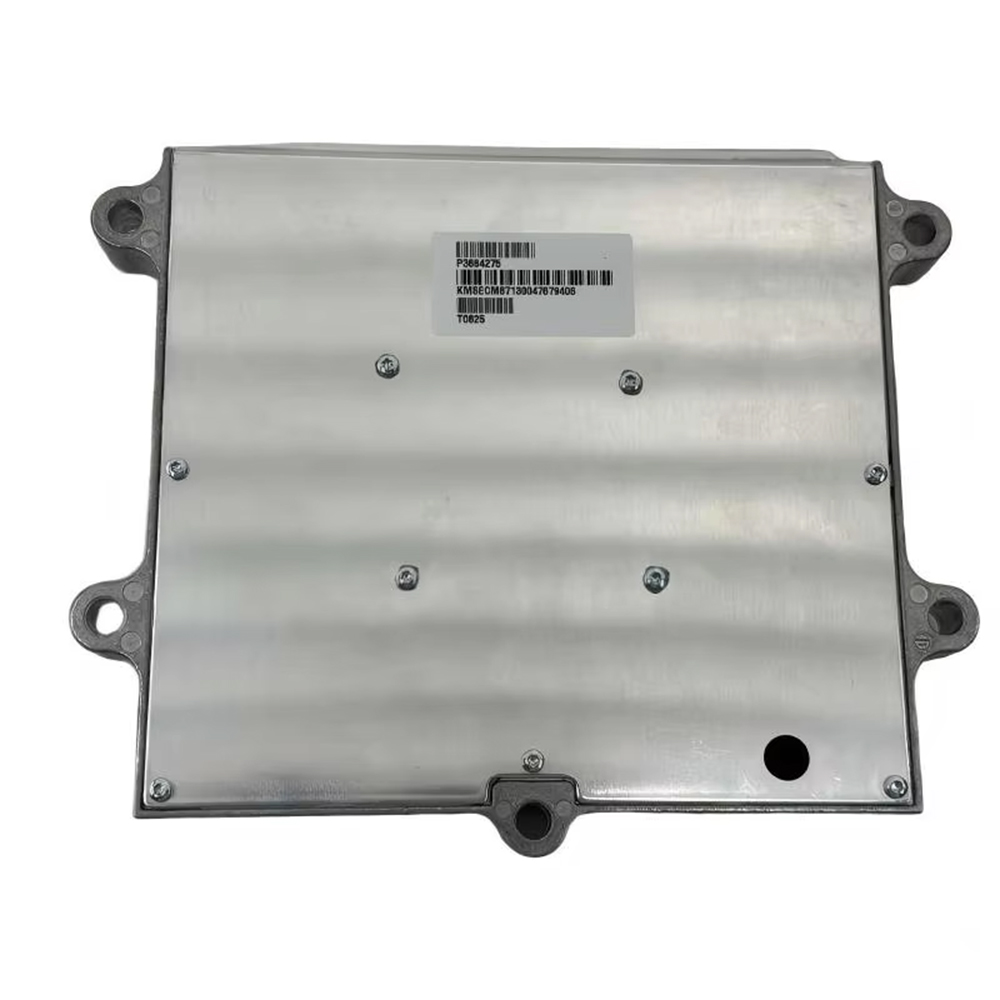
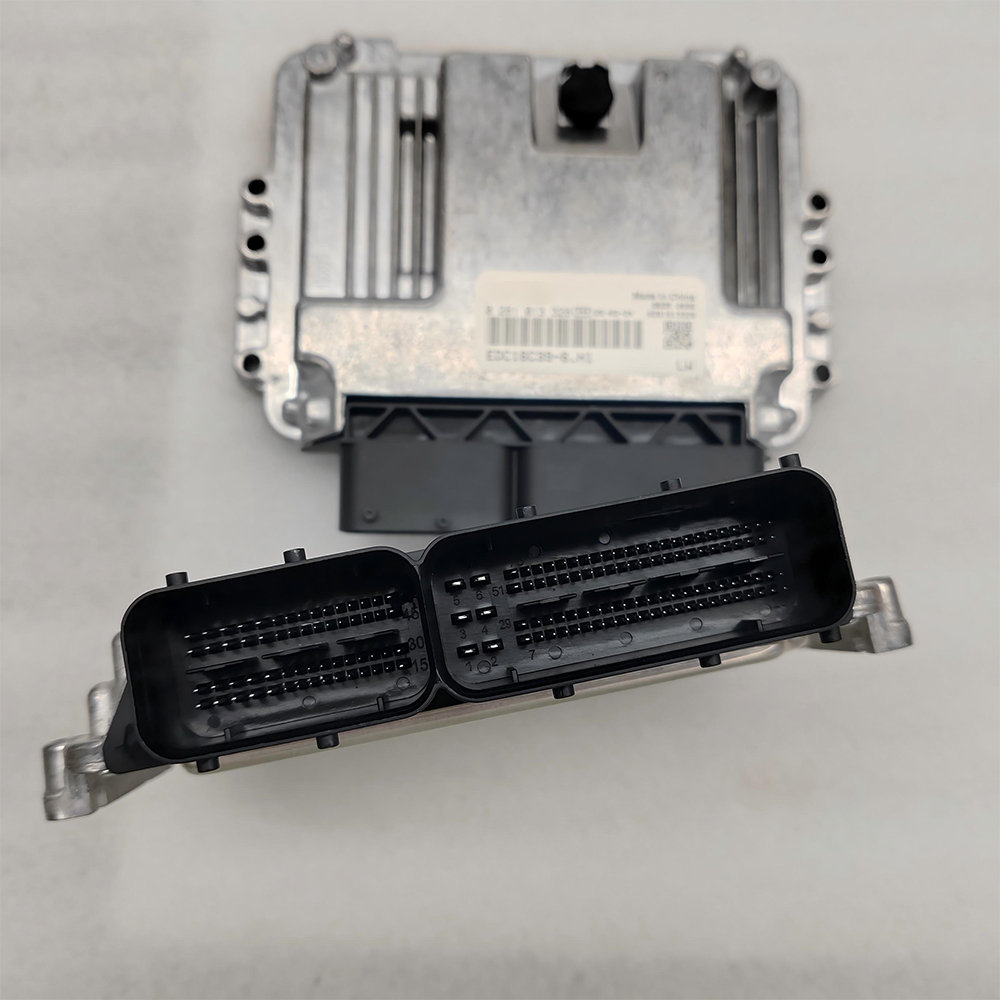
| Hechuang Technology (Wuxi) Co., Ltd.
|
Client
|
Model
|
Mercedes-Benz pump internal mainboard
|
||||||
| Test Report | Issue Date:
March 26, 2026 |
||||||||
| General Description:
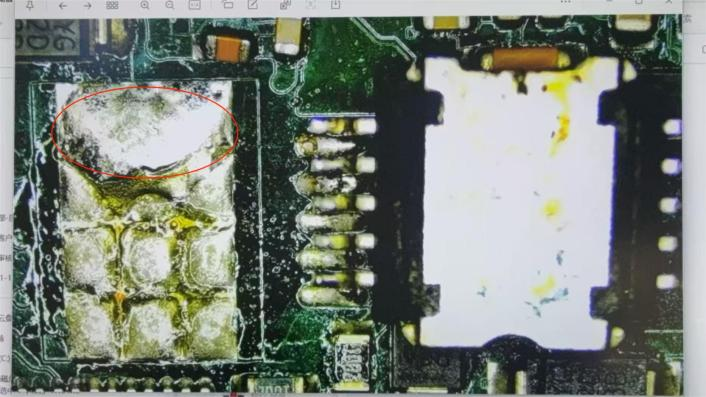
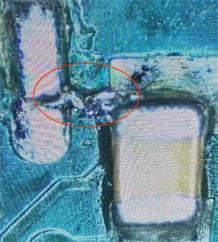
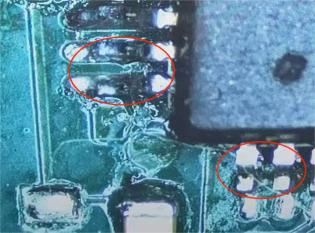
A cold solder joint was found on the dual-channel power driver chip at the client’s PCBA, causing product malfunction. Model Name: HC-PCB-B001 Quantity: 2500 PCS
|
|||||||||
| D1 Establish Problem Analysis Team Members | D2 Detailed Problem Description | ||||||||
| PIE:Sun Luyuan | The client detected a cold solder joint.
|
||||||||
| 品质:Ma Qianli | |||||||||
| 生产:Zhang Changping | |||||||||
  |
|||||||||
| D3 – Implement Temporary Corrective Actions | |||||||||
| 1. Arrange for personnel to promptly retrieve problematic products from the customer’s location.
2. The Quality Department should re-inspect work-in-process on the production line, focusing on these types of defects. |
|||||||||
| D4 – Root Cause Analysis | |||||||||
| The main root cause is that the PCBA and IC did not go through the reflow oven. During SMT mounting, the IC’s grounding pad was exposed to air for an extended period. The surface may have undergone oxidation reactions, forming a thin oxide film that made soldering difficult during the mounting process, ultimately resulting in cold solder joints after product completion. When testing products on the test bench, the short testing time made it difficult to detect cold solder joint issues. After the customer installed and tested the products, uncertainties in environmental and temperature factors revealed non-conforming products. The power chip’s unstable power supply due to cold solder joints caused EEPROM chip data errors, resulting in abnormal product operation. | |||||||||
| D5 – Define and Verify Root Corrective Actions | |||||||||
| 1. Train surface mount technology (SMT) technicians to promptly modify process flows and improve component storage locations and environments.
2. Develop prototyping and production sampling plans, and carefully inspect for issues such as missing solder joints, cold solder joints, and bridging. |
|||||||||
| D6 – Implement and Track Root Corrective Actions | |||||||||
| 1. Test operators shall extend testing time when conducting product qualification tests.
2. Repair items must follow the repair item process and undergo repeated testing and inspection. |
|||||||||
| D7 – Preventive Measures to Avoid Recurrence | |||||||||
| 1. Strictly regulate SMT processes; SMT personnel must strictly follow procedures and conduct disassembly inspections on SMT products.
2. Quality inspection shall conduct 100% full inspection on repaired items. |
|||||||||
| Reported by | Ma Qianli | Approved | Reviewed | Sun Luyuan | |||||
 English